A large capacity refrigerated centrifuge manufacturer is based on a combination of speed, pressure, and design geometry. The development of more advanced rotor designs has optimized airflow and reduced heat generation when operating. Programmable memory is featured in most systems, allowing users to store frequently used parameters to maximize efficiency. Additionally, power-saving motors and sound-dampening enclosures minimize lab discomfort. The ability to spin micro and macro volumes with the same reproducibility gives large capacity refrigerated centrifuge manufacturer equipment an edge both in the research and industrial settings. As technology advances, it remains to be at the forefront of precision and productivity.

large capacity refrigerated centrifuge manufacturer technology is a principal component in diverse manufacturing processes. In wastewater treatment, large capacity refrigerated centrifuge manufacturer assist in separating sludge from liquids to improve recycling efficiency. In the manufacture of cosmetics, large capacity refrigerated centrifuge manufacturer facilitate even emulsion and cream mixing. Crop research facilities apply it to analyze soil nutrients and plant extracts. It is also used in the manufacture of vaccines through the purification of viral particles and protein fractions. Through the ability to adapt to many substances and work requirements, large capacity refrigerated centrifuge manufacturer continues to support industries seeking consistency, purity, and scalability.
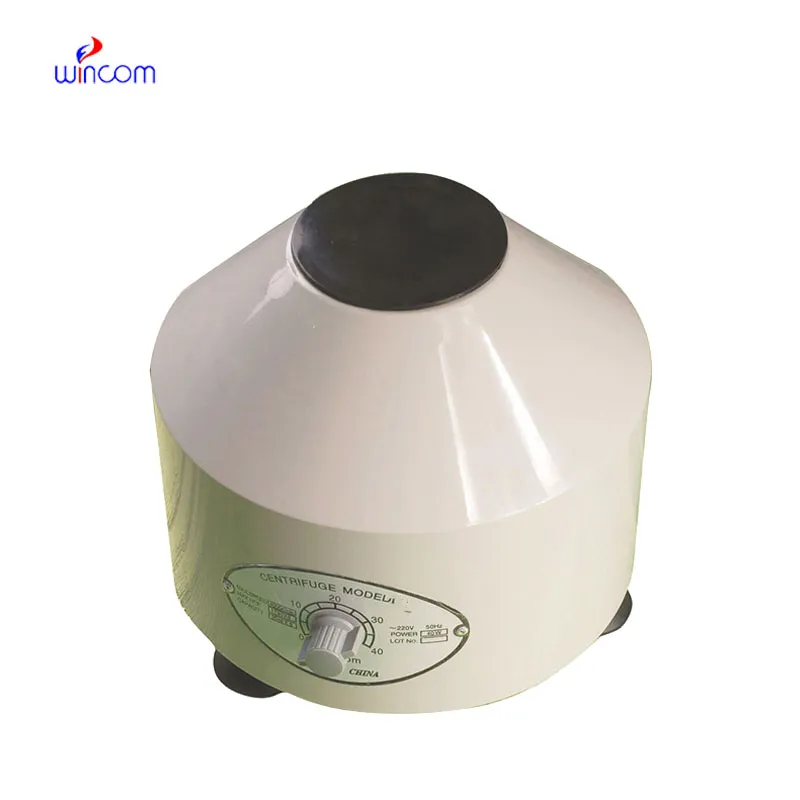
Future development of large capacity refrigerated centrifuge manufacturer will focus on precision control and data integration. Next-generation models will have sophisticated sensors that log every parameter of operation, generating total digital records for traceability. Performance trends will be predicted using machine learning, providing repeatable results. Hybrid large capacity refrigerated centrifuge manufacturer systems that can perform solid-liquid-gas separations will become a reality. Better safety designs and noiseless operation will make them easier to use. As research demands grow, these intelligent, automated large capacity refrigerated centrifuge manufacturer will be at the center of labs, enabling faster discovery and industrial productivity globally.
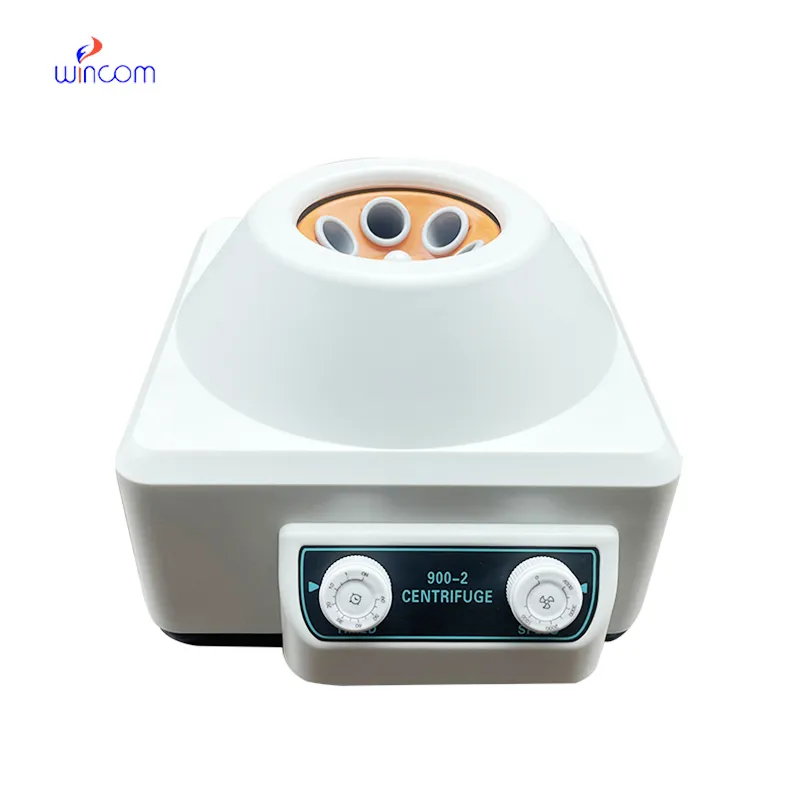
For long-term efficiency, large capacity refrigerated centrifuge manufacturer must be maintained with thorough attention to detail of operation. Every rotor and adapter must be checked for integrity before sample loading. After every cycle, the apparatus needs to be washed with neutral detergents and dried thoroughly. Vibration and mechanical stress are prevented by regular tests of balance. Seals and filters need to be replaced according to service schedules. Dust deposition is prevented by keeping the instrument in a covering when not used. If large capacity refrigerated centrifuge manufacturer apparatus is cared for according to disciplined procedure, equipment will give consistent high-performance performance year in year out.
The large capacity refrigerated centrifuge manufacturer is an essential instrument in science and engineering. It is able to separate material constituents based on their differences in density by rotating them at very high speeds. In biotechnology, it is used to purify cells, DNA, and enzymes. In chemistry, it purifies liquids and removes impurities from them. large capacity refrigerated centrifuge manufacturer also play a crucial role in medical diagnosis when preparing blood samples. Their mechanical precision and regulation of speed ensure safe use. Constantly enhanced design and electronic monitoring system development enhances efficiency, and large capacity refrigerated centrifuge manufacturer are thus inevitable in numerous modern applications.
Q: What factors affect the performance of a centrifuge? A: Performance depends on rotor design, speed accuracy, load balance, and regular maintenance of mechanical and electrical parts. Q: How should a centrifuge be cleaned? A: Use a soft cloth and mild detergent to clean the chamber and rotor, avoiding abrasive or corrosive substances that could cause damage. Q: Can a centrifuge be used for temperature-sensitive samples? A: Yes, refrigerated models are designed to maintain stable temperatures, protecting samples from heat generated during rotation. Q: What does RPM mean in centrifuge operation? A: RPM stands for revolutions per minute, indicating how fast the rotor spins—higher RPMs generate stronger centrifugal forces. Q: When should the rotor of a centrifuge be replaced? A: Rotors should be replaced when signs of fatigue, corrosion, or cracking appear, or after reaching the manufacturer’s specified lifespan.
The microscope delivers incredibly sharp images and precise focusing. It’s perfect for both professional lab work and educational use.
The hospital bed is well-designed and very practical. Patients find it comfortable, and nurses appreciate how simple it is to operate.
To protect the privacy of our buyers, only public service email domains like Gmail, Yahoo, and MSN will be displayed. Additionally, only a limited portion of the inquiry content will be shown.
We’re currently sourcing an ultrasound scanner for hospital use. Please send product specification...
Hello, I’m interested in your centrifuge models for laboratory use. Could you please send me more ...
E-mail: [email protected]
Tel: +86-731-84176622
+86-731-84136655
Address: Rm.1507,Xinsancheng Plaza. No.58, Renmin Road(E),Changsha,Hunan,China


 EN
 af
 es
 ar
 tr
 sw
 pt
 th
 ur
 bn
 ne
 vi
 km
 lo
 de
 ru
 fi
 nl
 fa
 fr
 ko